Leave Your Message
-
Phone
-
E-mail
-
Whatsapp
-
WeChat
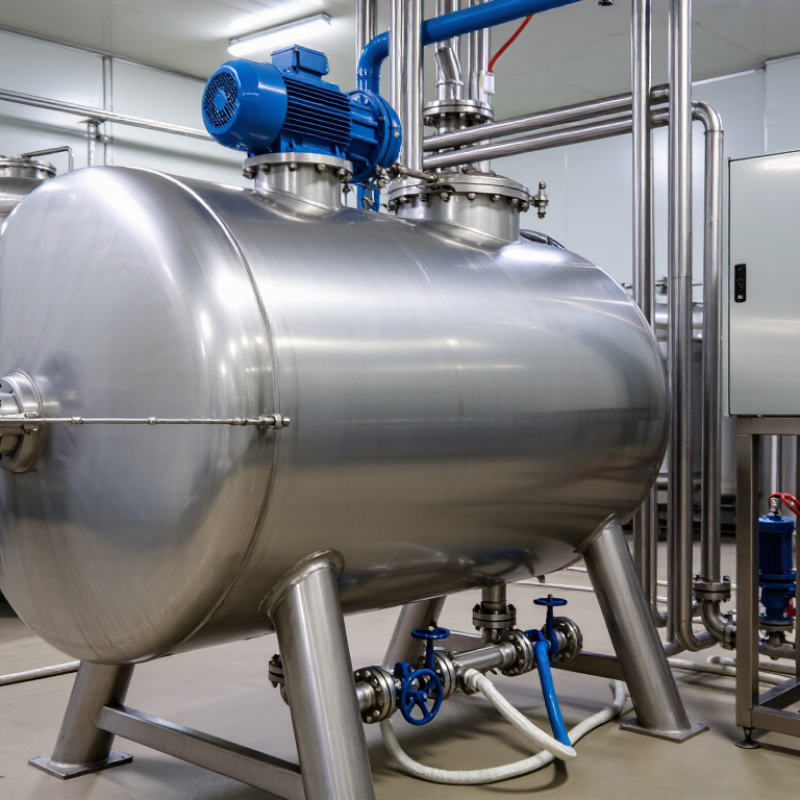
Choosing a mixing tank is not just a matter of capacity or price. The right vessel must suit your ingredients, process, cleaning routine, and production goals. Stainless Steel Mixing Tanks are used across many industries, but their design and materials vary considerably. A tank that works well for a thin liquid may struggle with a thick, heat-sensitive batch.
Start with the product and the process. Consider batch volume, viscosity, operating temperature, and whether ingredients need gentle blending or stronger agitation. A small sample batch can reveal issues that a specification sheet may not show. Watch how powders disperse, whether solids settle, and how much residue remains near the tank bottom. Small details matter.
Material selection deserves careful attention. Stainless steel grade, surface finish, weld quality, and seal materials can affect corrosion resistance and cleanability. Confirm compatibility with the actual ingredients and cleaning chemicals, rather than relying on broad labels such as “food-grade.” Also check impeller type, clearance, motor controls, and any heating or cooling jacket. These choices influence mixing performance and operating costs.
There is no perfect tank for every application. Requirements can change as recipes, batch sizes, or production schedules evolve. Some assumptions will need a second look. This guide explains the main factors to compare when choosing a stainless steel mixing tank, including capacity, construction, agitation, temperature control, and maintenance. Use it to frame practical questions for suppliers and evaluate options against your real operating conditions—not just the brochure.
How to Choose a Stainless Steel Mixing Tank
Define the Product, Process, and Operating Requirements
Start with the product, not the tank catalogue. Record each ingredient’s pH, chloride content, temperature, viscosity, and abrasive solids. These details influence steel grade, seal selection, and agitator design. A mildly acidic liquid and a salty brine can behave very differently. World Stainless reported 58.4 million tonnes of global stainless-steel melt-shop production in 2023. That figure shows the material’s broad industrial use, but it does not prove that every stainless grade suits your process. Confirm compatibility with a qualified materials specialist.
Next, map the actual operating cycle: batch volume, mixing time, heating or cooling needs, cleaning method, and expected shear. A thick paste may need a different impeller and motor than a thin solution. Check access for inspection, drainage, and cleaning; residue can collect around nozzles and welds. Include working pressure, vacuum exposure, and available utilities in the specification. One easy mistake is sizing only for normal production. Startup and cleaning conditions may be tougher. I would revisit the specification after a trial batch, because real flow can surprise even an experienced team.
Tips: Write down the smallest and largest batch sizes. Note product temperature and cleaning chemicals. Ask the supplier to document material grade, surface finish, and weld inspection. Keep a sample of the product for compatibility testing. Small detail. Big difference.
| Requirement | What to Define | Example Data or Starting Point | Why It Matters for Tank Selection |
|---|---|---|---|
| Product and ingredients | List every ingredient, concentration, pH range, and any corrosive or abrasive components. Identify whether the batch is food, beverage, cosmetic, pharmaceutical, or industrial product. | For example: an aqueous product with mild organic acids, a stated pH range, and no abrasive solids. Confirm compatibility against the complete formulation and operating conditions. | Corrosion resistance depends on the specific chemistry, concentration, temperature, and exposure time—not just the product category. |
| Wetted material | Specify the material for all product-contact parts, including the vessel, agitator, baffles, nozzles, and fittings. | Type 304L stainless steel is commonly considered for many general-purpose applications. Type 316L is often evaluated where greater resistance to chlorides or certain chemicals is needed. | Neither grade is suitable for every formulation. Verify material compatibility with a qualified materials specialist, especially for chloride-bearing or acidic products. |
| Batch and working volume | Define the smallest and largest batch, required usable volume, and whether the stated capacity is working volume or total vessel volume. | A preliminary planning estimate may place working volume around 70–85% of gross vessel volume; foaming, vortexing, heat expansion, and headspace requirements can change this range. | Correct sizing provides room for mixing and process expansion while reducing overflow risk. Confirm usable volume with the actual process and tank geometry. |
| Viscosity and flow behavior | Record viscosity at relevant process temperatures, whether the product is shear-thinning or shear-thickening, and whether it contains suspended solids. | State measured viscosity in mPa·s (cP) at a specified temperature and, for non-Newtonian products, at a specified measurement condition or shear rate. | Viscosity and flow behavior influence impeller type, motor power, shaft design, mixing time, and whether additional wall-sweeping action is needed. |
| Mixing objective | Describe the required result: blending liquids, dissolving powders, suspending solids, dispersing ingredients, or maintaining a uniform temperature. | Define a measurable target where possible, such as a specified blend uniformity or a maximum mixing time for a stated batch size. | Different tasks require different impeller designs and operating speeds. A high-speed disperser is not automatically the best choice for every blending duty. |
| Agitator configuration | Specify preferred impeller style, shaft arrangement, baffles, drive location, and any need for variable speed or multiple mixing elements. | Axial-flow impellers are often considered for bulk circulation; radial-flow impellers may be used for dispersing or high-shear duties. Final selection depends on the product and vessel geometry. | Agitator geometry affects circulation, shear, solids suspension, vortex formation, and motor load. Request process-based sizing rather than selecting by motor power alone. |
| Temperature and heat transfer | Define normal and maximum product temperatures, heating or cooling rates, allowable temperature variation, and the heat-transfer medium. | State the required operating range and whether heating or cooling will use a jacket, half-pipe coil, internal coil, or an external heat exchanger. | Temperature limits affect vessel design, seals, insulation, jacket selection, and the risk of product scorching or slow batch cycles. |
| Pressure and vacuum | Identify whether the tank operates at atmospheric pressure, under vacuum, or with positive pressure, and define the required design conditions. | Provide maximum operating pressure and vacuum in the units used at the site, plus the applicable jurisdictional code and inspection requirements. | A tank intended for atmospheric service should not be assumed suitable for pressure or vacuum. The vessel, closures, fittings, and relief protection must be designed for the specified conditions. |
| Cleanability and surface finish | Define manual or automated cleaning, cleaning chemicals, rinse requirements, drainability, and hygienic design expectations. | A product-contact surface finish of Ra ≤ 0.8 μm is a commonly specified starting point in some hygienic applications, but the required finish depends on the product and applicable standards. | Surface finish, weld quality, internal crevices, spray-device coverage, and outlet geometry influence cleaning effectiveness and residue removal. |
| Sanitary features | Specify required fittings, sample points, manway access, gasket materials, drain design, and documentation or validation needs. | For hygienic service, define product-contact gasket compatibility, cleanable connections, and whether cleaning-in-place (CIP) coverage must be demonstrated. | Appropriate details support repeatable cleaning and inspection. Requirements vary by industry, product risk, and local regulations. |
| Solids, powders, and additions | State solids concentration, particle size, settling tendency, powder addition rate, and whether ingredients must be added during mixing. | Describe the addition method, such as a top manway, dedicated charging port, or powder-induction system, and identify dust-control needs. | Inlet location and agitator performance affect wetting, clumping, dust exposure, and the ability to keep solids suspended. |
| Installation and utilities | Measure available floor space, door and ceiling clearances, floor loading, power supply, and utility connections. | Provide the site voltage and frequency, available heating or cooling utilities, access route, and required operating clearances. | Physical and utility constraints can affect tank orientation, motor selection, service access, installation cost, and commissioning. |
| Controls and instrumentation | Define required monitoring and control for speed, temperature, level, pressure, batch timing, and alarms. | List required instruments, control interface, data-recording needs, and any plant communication or automation requirements. | Controls should match the process risk and operating procedure. Instrument ranges and wetted materials must suit the product and conditions. |
| Safety and compliance | Identify applicable pressure-vessel, electrical, food-contact, workplace, and site requirements before specifying the equipment. | Provide the installation country or region, hazardous-area classification if applicable, and required design or inspection standards. | Regulatory obligations depend on location, service, and equipment design. Confirm requirements with the responsible engineering and compliance teams. |